

Industrial DeNOx projects rarely fail because engineers do not understand the basic SCR reaction. The more difficult issue is deciding where the SCR reactor should sit in the existing process and what the catalyst will actually be exposed to at that location.
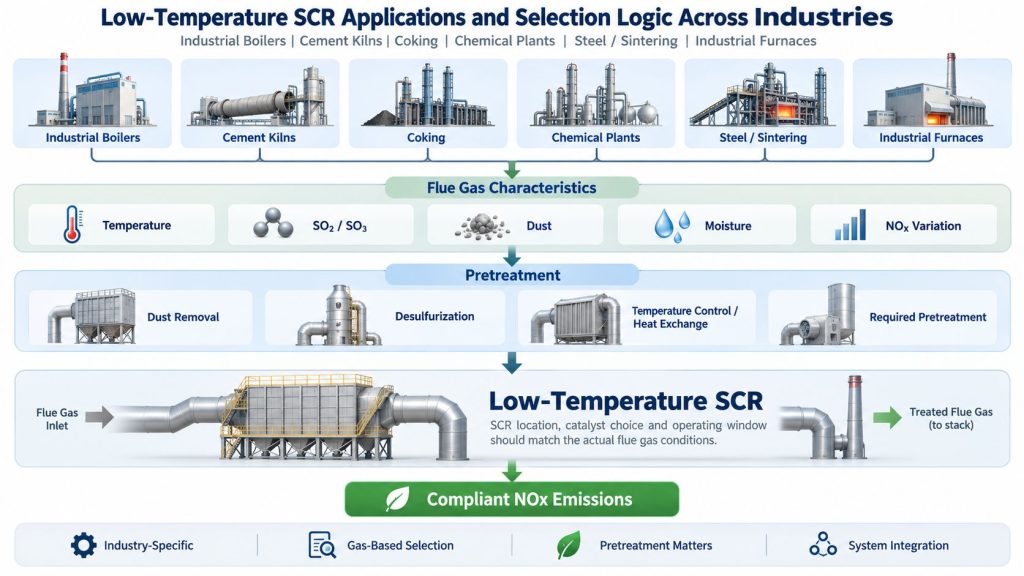
An industrial boiler, cement kiln, coke oven, sintering line and chemical process may all require NOx control, but their flue gas conditions are very different. Temperature, SO₂/SO₃, particulate loading, moisture, process variability and the existing pollution-control train can all change the appropriate SCR configuration.
There Is No Universal SCR Configuration for Industrial DeNOx
The U.S. EPA’s Chapter 2 – Selective Catalytic Reduction describes SCR applications across a wide range of stationary sources, including industrial boilers, process heaters, chemical plants and steel mills. It also distinguishes between high-dust, low-dust and tail-end SCR arrangements.
That distinction is important in industrial projects. Locating an SCR reactor in a hotter section of the process can provide favorable reaction temperature, but the catalyst may be exposed to more dust, sulfur species and potential poisons. Moving the reactor downstream of particulate and sulfur control can provide a cleaner gas stream, but the available temperature may then be much lower.
Low-temperature SCR can provide additional process flexibility where the downstream gas temperature is still suitable for catalytic NOx reduction. Its value is not simply “operating at a lower temperature,” but reducing the need to reheat a large flue-gas stream solely to satisfy the catalyst temperature window.
Where Is SCR Used in Industrial NOx Control?
| Industry | Typical Flue Gas | Temperature Profile | Key Risks | SCR Selection Focus |
|---|---|---|---|---|
| Industrial Boilers | Strongly dependent on fuel; natural gas is relatively clean while biomass may introduce more dust and alkali species | Often significantly cooler after heat recovery | Low-load temperature, reheating demand and fuel variability | Available tail-end temperature, minimum operating condition and fuel-related contaminants |
| Cement Kilns | High gas flow with significant particulate loading and complex raw-material chemistry | Changes with raw mill, heat recovery and particulate-control operation | Dust, SO₃, plugging and catalyst deactivation | Reactor location, dust removal, sulfur exposure and long-term stability |
| Coke Ovens | NOx, SO₂, moisture and particulate matter may need to be considered together | Can enter a medium- or low-temperature range after heat recovery and upstream treatment | Sulfur exposure, ammonium salt deposition and temperature variation | FGD/SCR sequence, inlet sulfur load and available SCR temperature |
| Steel / Sintering | Large gas volumes with dust, SO₂ and NOx | Depends heavily on the existing treatment train | Particulate deposition, sulfur effects and catalyst contamination | Integration of particulate control, desulfurization and SCR |
| Chemical Processes | Highly process-specific gas composition | May vary substantially with production load and operating state | Catalyst poisons and rapid composition changes | Full gas analysis rather than temperature alone |
| Industrial Furnaces and Kilns | Dependent on furnace type, fuel and production cycle | Often varies with load | Temperature excursions, dust and sulfur fluctuations | Stable catalyst window, reactor location and potential reheating |
Industrial Boilers: Tail-End Temperature Is Often the Main Constraint
For many industrial boilers, the most practical SCR challenge appears after heat recovery. The furnace may provide more than enough temperature, but by the time the flue gas reaches the downstream emissions-control section, the temperature can be considerably lower.
If conventional SCR requires substantial reheating of the full gas stream, fuel consumption and retrofit complexity increase. Low-temperature SCR may therefore be evaluated where the existing tail-end temperature can be used more effectively.
Fuel still matters. Natural-gas-fired boilers generally present a cleaner flue gas than biomass boilers, while biomass applications may require greater attention to particulate matter, alkali species and fuel variability. See Low-Temperature SCR DeNOx for Natural Gas and Biomass Boilers: Process Design and Catalyst Selection for a detailed comparison.
Cement and Coking: Dust, Sulfur and Process Integration Matter Together
Cement-kiln SCR selection begins with reactor location. Raw-mill operation, heat recovery and particulate control can significantly change both temperature and gas composition before the flue gas reaches the catalyst. Dust loading and SO₃ exposure also affect long-term catalyst performance. For a detailed process discussion, see Low-Temperature SCR for Cement Kiln Flue Gas: Process Design, Temperature Window and Catalyst Selection.
Coke oven projects present a different integration problem. SO₂ removal, NOx control and the available temperature should often be evaluated as one treatment train rather than as separate equipment packages. Where sulfur loading remains significant before a low-temperature SCR reactor, SOx, moisture and ammonia can create additional deposition risks. See Desulfurization and Low-Temperature SCR DeNOx for Coke Oven Flue Gas.
Steel sintering presents a similar system-level issue because large gas volumes may contain NOx, SO₂ and particulate matter simultaneously. In these applications, the SCR inlet condition should be established only after the existing particulate-control, desulfurization and heat-recovery arrangement is understood. See Ultra-Low-Temperature SO₂ and NOx Removal Using Catalytic FGD and SCR for the broader integrated treatment concept.
Chemical Plants and Industrial Furnaces: Operating Variability Can Matter More Than One Temperature Number
Chemical process off-gas and industrial furnace exhaust cannot be characterized by one typical condition. Normal operation may place the gas inside the catalyst temperature window, while startup, shutdown, production-rate changes or feedstock changes can move both temperature and composition outside the preferred range.
Chemical applications also require attention to process-specific compounds that may affect catalyst activity. Industrial furnaces used in glass, ceramics, metallurgy and other manufacturing processes may introduce different dust, sulfur and fuel-related contaminants.
For these applications, a single “normal operating temperature” is not enough for catalyst selection. Minimum and maximum temperature, the duration of off-design conditions and the corresponding gas composition provide much more useful engineering information.
How Can You Determine Whether an Existing Flue Gas Is Suitable for Low-Temperature SCR?
Temperature
Use the actual temperature at the proposed SCR inlet rather than furnace-outlet temperature. Minimum-load temperature and the duration of low-temperature operation are particularly important for retrofit projects.
SO₂ and SO₃
Low-temperature operation increases the importance of sulfur management. SOx, moisture and ammonia can contribute to ammonium salt formation, so sulfur loading at the catalyst inlet must be considered when deciding whether upstream desulfurization is required.
Particulate Matter
Dust concentration, particle size and composition influence catalyst plugging, erosion and pressure drop. A high-dust arrangement cannot be evaluated in the same way as a low-dust or tail-end SCR system.
Moisture
Moisture should be evaluated together with sulfur species, dew point and minimum operating temperature. Condensation or prolonged wet operation can create additional problems in low-temperature sections of the system.
NOx Concentration and Variation
Average NOx concentration alone is not sufficient. Peak inlet concentration, load variation and required outlet emissions affect catalyst volume, ammonia dosing and control range.
Available Space and Pressure Drop
Retrofit projects are often limited by existing ductwork, fan capacity and installation space. Even where catalyst chemistry is suitable, the reactor design may need to change if the plant cannot accommodate additional pressure drop or a conventional reactor footprint.
Application Range of DAQI Low-Temperature DeNOx Technology
DAQI Technology’s current low- and ultra-low-temperature SCR platform can be evaluated across an overall DeNOx temperature range of approximately 90–180°C. Potential applications include industrial boilers, coking, cement, iron and steel, industrial furnaces and selected chemical-process exhaust streams.
The 90–180°C range refers to DAQI’s overall current DeNOx technology platform. It should not be interpreted as a guaranteed operating range for every flue gas, and the operating range of an individual N-101 or N-201 catalyst grade should not be used to define the capability of the complete technology platform.
Final catalyst selection, space velocity, reactor volume, operating temperature and pretreatment requirements depend on SO₂, SO₃, particulate loading, moisture, O₂, NOx, gas flow and the required outlet emission level. For the underlying technology and catalyst-selection principles, see Low-Temperature SCR DeNOx Technology for Industrial NOx Control.
What Flue-Gas Data Are Needed for an Initial SCR Assessment?
| Parameter | Recommended Data |
|---|---|
| Flue Gas Flow | Normal, minimum and maximum flow in Nm³/h |
| Temperature | Normal, minimum and maximum temperature at the proposed SCR location |
| NOx | Average inlet, peak inlet and required outlet concentration |
| SO₂ / SO₃ | Raw-gas concentration and residual sulfur after existing FGD |
| Particulate Matter | Concentration, major composition and existing dust-control system |
| Moisture | Water content, condensation risk and relevant dew-point information |
| O₂ and Other Components | O₂, CO and any process-specific compounds or potential catalyst poisons |
| Existing Treatment Train | Current sequence of heat recovery, particulate control, desulfurization, fans and stack |
| Site Constraints | Available installation space, allowable pressure drop, heat source and shutdown limitations |
These data are normally sufficient for a first-stage assessment of whether low-temperature SCR is technically relevant. For retrofit projects, an existing process flow diagram is also valuable because the final solution is often determined not only by catalyst activity, but by how the SCR system can be integrated into the plant without disrupting the existing production and emissions-control process.